A filler primer is a thick spray primer that fills fine scratches and shallow layer lines and sands flat, while a regular primer only gives paint something to grip. Neither one fixes deep layer lines or gaps, so the reliable route to a smooth surface is: fill the big defects with putty or body filler, sand, spray a filler primer as a guide coat, sand again, and repeat until the primer shows no flaws. Prusa finishes painted parts with P400 paper, and Rust-Oleum’s filler primer data sheet says to let the coat dry 2 to 4 hours before dry sanding (wet sanding can start as soon as it is dry to the touch, about 10 minutes at 70 °F / 21 °C).
This guide explains what each product does, how to combine them, how to prime PLA, PETG, ABS and resin, and how to fix runs, orange peel, poor adhesion and the other flaws primer shows. Product numbers come from the manufacturers’ data sheets and tutorials linked at the end. Grits for repairs that no maker publishes are labelled as starting points. Sanding technique has its own guide, and painting starts after this one.
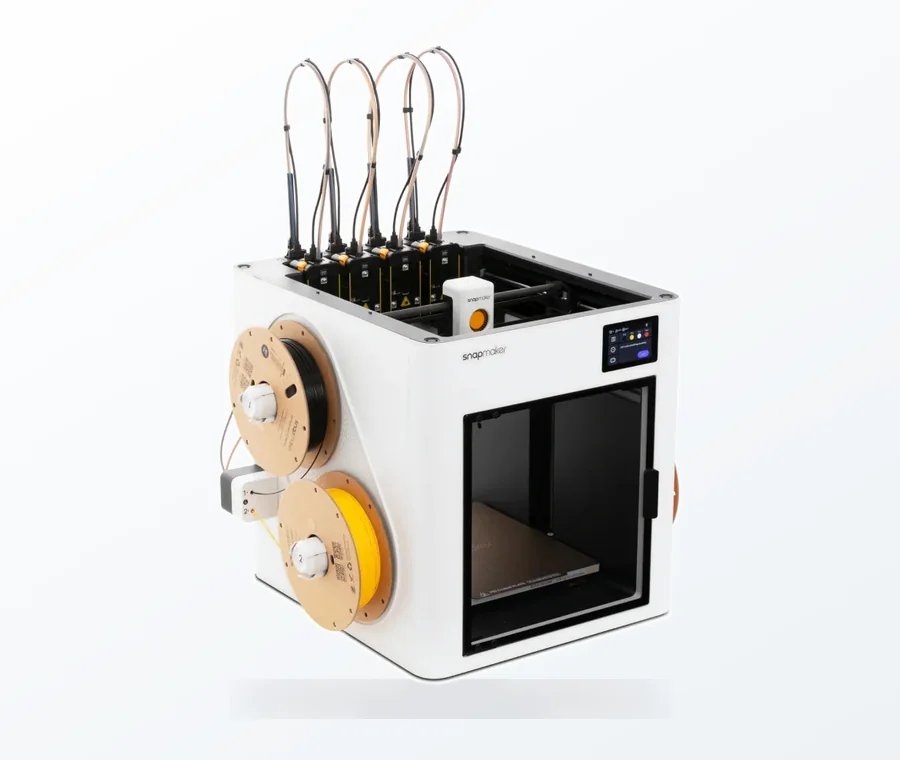
The consumer toolchanger 3D printer: the SnapSwap 4-toolhead system swaps heads in 5 seconds for true multi-color and multi-material printing, with smart calibration and auto filament loading.
- 4 toolheads · 5 s swap
- Up to 500 mm/s · 20,000 mm/s²
- 270 mm cube build volume
- Multi-color & multi-material
Smooth surface in seven steps
- Clean the print, remove supports and trim blobs. Sanding is slow at removing lumps.
- Fill gaps and deep pits with body filler or putty. Let it cure fully.
- Sand level, around P100 to P220 for FDM (see the grit progression guide).
- Spray a light coat of filler primer. The uniform color shows every dip and scratch.
- Mark the flaws, fill the small ones with spot putty, and sand again.
- Repeat primer, mark and sand until the surface looks flat under raking light. Sand with P400 before the last coat, the grit Prusa uses on painted parts.
- Spray a final thin coat of primer, then start painting.
Which product does what
Primer, filler and coating are three different jobs. A thick coat of the wrong one hides detail without hiding the layer lines.
| Product | What it is for | Data from the maker |
|---|---|---|
| Fine hobby primer (Vallejo Surface Primer, Tamiya Fine Surface Primer L) | Adhesion and an even base color on small, detailed models; almost no filling | Vallejo: sandable wet or dry; Tamiya: spray primer for plastic and metal |
| Filler primer (e.g. Rust-Oleum Filler Primer) | Fills minor imperfections, sands flat | Dry to touch in 10 minutes at 70 °F / 21 °C and 50 % humidity; 2 to 4 hours before dry sanding; 1.5 to 2.5 mils (37.5 to 62.5 µm) dry film per coat |
| Two-part body filler (e.g. Bondo Original Filler) | Gaps, deep layer lines, big repairs | 3 to 4 minutes of working time once mixed; sands after 20 minutes; rough shape at 80 grit, finish with 180 and finer |
| Glazing or spot putty | Pinholes and small scratches left after the first primer | Bondo’s filler sheet says to use it on small imperfections, then re-prime with 2 to 3 coats |
| Epoxy brush-on coating (XTC-3D) | Fills layer lines over the whole surface in one coat | Mix 2A:1B by volume; 10 minutes pot life; tack-free about 2 hours at 73 °F / 23 °C |

Check the can before buying. Rust-Oleum’s data sheet for its Filler Primer lists metal, wood and fiberglass as the surfaces it is made for, not plastic, so test it on a scrap print first. Tamiya markets its fine primer for plastic and metal, and Vallejo’s tutorials show its primer on both plastic and resin models.
Filling gaps and layer lines before priming
Primer shrinks back into deep valleys as its solvent evaporates, and each coat adds thickness. If every coat reaches the recommended 1.5 to 2.5 mils, three coats of Rust-Oleum’s filler primer add roughly 0.11 to 0.19 mm to each surface, which already softens fine detail (simple arithmetic from the data sheet figure). So fill first, then prime.
- Body filler for gaps and deep lines. Bondo’s data sheet gives 3 to 4 minutes of working time, and a 3 in (about 7.5 cm) strip of hardener for a 3 in puddle of filler as the maximum batch. Spread a thin first layer with firm pressure, shape it with 80 grit and finish at 180 and finer. Prusa uses P100 on its body filler and repeats thin layers until the gaps are not visible.
- Spot or glazing putty after the first primer coat, for pinholes. Prusa also uses putty to hide places where sanding went through to the infill.
- Epoxy coating when you want the whole surface smoothed without sanding every line. Smooth-On’s XTC-3D is brushed on as one thin layer, under 1/64 in (about 0.4 mm), with a foam brush, and cures in about 3.5 to 4 hours. It works on PLA, ABS and SLA prints, the cured coat can be sanded and primed, and the maker lists a NIOSH-approved respirator for sanding and no glass or foam mixing cups because the mix gets hot.
Reducing the work upstream also helps: a smaller layer height and a well-placed seam leave less to fill. The slicer side is covered in eliminating visible layer lines, and ABS and ASA can skip filler entirely with acetone vapor smoothing.
Priming step by step
- Wash and dry. Wash with soap and water or wipe with IPA, and let the part dry fully. Resin parts must be washed and cured first; see washing and curing resin.
- Scuff glossy surfaces. Rust-Oleum’s data sheet says to lightly sand glossy surfaces, which is relevant to glossy PETG and resin.
- Check the conditions. Rust-Oleum specifies 50 to 90 °F (10 to 32 °C) and humidity below 85 %, with dry times based on 70 °F and 50 %. Cooler air needs longer.
- Shake or swirl as the can says. Rust-Oleum says to shake for a minute after the ball rattles. Formlabs’ guide advises swirling for 2 to 3 minutes instead of shaking, to avoid propellant bubbles. The label wins.
- Spray in light passes. Rust-Oleum says 12 to 16 in (30 to 40 cm) and two or more light coats a few minutes apart. Prusa sprays from about 20 cm at a shallow angle of about 15 degrees, and Formlabs uses 6 to 8 in (15 to 20 cm) in short strokes. These are different products, so follow your can. Start and end each stroke off the part.
- Inspect, then sand. Mark the flaws with a marker (Prusa notes alcohol-based markers do not show through paint), sand with fine paper (Formlabs: finer than 600 grit; Prusa: P400), wipe off the dust and respray.
- Wait. Follow the can before sanding or painting. For Rust-Oleum that is 2 to 4 hours before dry sanding.
A heavy primer can replace some sanding, but Formlabs warns it may obscure intricate details. On small, detailed parts use a fine hobby primer in thin coats. Vallejo’s Surface Primer sands wet or dry without peeling, produces a fine dust (wipe it off before repriming) and the airbrush must be cleaned straight after use.
Primer by material
| Material | Prep | Watch out for |
|---|---|---|
| PLA | Sand wet or slowly; Prusa says PLA softens above about 60 °C | Do not force-dry in a hot oven. Aerosol primers can contain strong solvents (Rust-Oleum’s lists acetone and aromatic hydrocarbons), and Prusa notes acetone can partially dissolve some PLA, so make the first coat a light mist |
| PETG | Sands well dry and wet (Prusa); glossy surface, so scuff it | Test adhesion on a scrap print before committing a finished part |
| ABS and ASA | Sand, or smooth with acetone vapor first | Same solvent caution as PLA on thin or small parts; acetone smoothing is covered in its own guide |
| Resin | Remove supports, sand the marks, wash and cure fully (Formlabs) | Uncured resin blocks adhesion. Use a fine primer in thin coats; Formlabs notes Tamiya goes on very thinly and evenly |
Fixing primer flaws
Primer exposes flaws on purpose, which means most of the “problems” are surface or technique issues. Let any flaw cure fully before touching it, because sanding wet primer smears.
| Flaw | Likely cause | Fix |
|---|---|---|
| Runs and sags | Too much primer in one pass, spraying too close or too slowly, cold air | Let it cure, sand flat (start around P400 to P600), clean the dust and respray in thin coats |
| Orange peel | Spraying too far or too close, air too hot or cold, paint applied too dry or not thinned enough to level (HMG Paint) | Wet sand flat with fine paper (around 800 to 1,200 is a starting point), polish if minor, recoat thinly |
| Gritty or rough surface | Dust, dry overspray | Sand lightly (around 600 to 800), wipe with a tack cloth and respray |
| Peeling or poor adhesion | Oil, dust or glossy surface; uncured resin; incompatible primer | Strip it back to bare plastic, wash, scuff, and re-prime with a plastic-compatible primer |
| Cracking or wrinkling | Coats too thick, applied before the last one dried, trapped solvent | Strip or sand back, then respray in thin coats with proper drying time |
| Bubbles or pinholes | Gas escaping from the print, vigorous shaking of aerosols (Formlabs), thick coat | Sand flat, fill pinholes with spot putty, respray in thin coats |
| Lost detail | Too many coats of a thick primer | Switch to a fine hobby primer; use as few coats as cover |
| Layer lines still visible | Primer cannot fill them | Fill or coat first (see the filler section), then reprime |
Grit values in the fix column are starting points, not manufacturer figures. Use the finest paper that removes the flaw, and check the primer maker’s guidance.
Safety and ventilation
Rust-Oleum’s data sheet says to use its filler primer outdoors or in a well ventilated area and not near an open flame. Bondo says to use its filler only with adequate ventilation and appropriate protective equipment for eyes, skin, respiratory system and hands, and Smooth-On lists a NIOSH-approved respirator for sanding cured XTC-3D. Sanding filler and primer produces fine dust, so wet sand where you can.
Common mistakes
- Expecting primer to fill deep layer lines. It sinks into valleys; fill them first.
- Priming before sanding. Filler primer is a tool for showing flaws, not a substitute for the first sanding pass. The sanding guide covers the order.
- One thick coat. It runs, traps solvent and fills detail. Two or more light coats are what the can asks for.
- Mixing incompatible products. Formlabs recommends a primer and paint from the same brand, both labelled for plastic.
- Skipping the test. A scrap print shows whether a solvent-based primer attacks your filament.
Once the primer is flat and dry, the next step is painting your print. If you are still choosing tools, the post-processing tools list covers sanding blocks and respirators.
Frequently asked questions
Do I need to sand a 3D print before using filler primer?
Yes, at least a first pass. Filler primer fills fine scratches and shallow lines, not ridges or gaps. Prusa roughs the part with P100, fills, then uses filler primer as a guide coat between sanding rounds and finishes with P400.
What is the difference between primer and filler primer?
A regular primer improves paint adhesion and gives an even base color. A filler primer is formulated thicker so it fills minor imperfections and can be sanded flat, at the cost of adding thickness (about 37.5 to 62.5 µm per coat for Rust-Oleum’s filler primer).
Can I use automotive primer on PLA?
Many people do, but check the can first. Rust-Oleum’s data sheet for its filler primer lists metal, wood and fiberglass, and its solvents include acetone, which Prusa says can partially dissolve some PLA. Spray a light first coat and test on a scrap print.
Why does my primer look rough or bumpy?
Rough primer usually comes from spraying too far away, dry overspray, dust or air that is too hot or too cold. Let it cure, sand lightly, wipe off the dust and respray thinner coats from the distance on the can.
Sources
- Rust-Oleum: Filler Primer technical data sheet (ATO-50)
- 3M Bondo: Original Filler technical data sheet (December 2023)
- Smooth-On: XTC-3D product page
- Prusa Research: Postprocessing of 3D prints step-by-step and PLA material guide
- Formlabs: How to prime and paint 3D printed parts, Vallejo: sanding primed surfaces and HMG Paint: orange peel